The operation of an large capacity refrigerated centrifuge manufacturer largely relies on its rotor design, accuracy in balancing, and operating speed. Modern models typically come with programmable interfaces that allow users to control acceleration rates, temperature, and run times with great accuracy. Some advanced large capacity refrigerated centrifuge manufacturer incorporate vibration sensing and auto-imbalances for stabilizing high-speed rotation. Additionally, the use of light but strong materials like carbon fiber enhances safety and energy efficiency. This marriage of engineering ingenuity and electronic control combines the large capacity refrigerated centrifuge manufacturer into a reliable partner for research and production environments.

large capacity refrigerated centrifuge manufacturer technology is a principal component in diverse manufacturing processes. In wastewater treatment, large capacity refrigerated centrifuge manufacturer assist in separating sludge from liquids to improve recycling efficiency. In the manufacture of cosmetics, large capacity refrigerated centrifuge manufacturer facilitate even emulsion and cream mixing. Crop research facilities apply it to analyze soil nutrients and plant extracts. It is also used in the manufacture of vaccines through the purification of viral particles and protein fractions. Through the ability to adapt to many substances and work requirements, large capacity refrigerated centrifuge manufacturer continues to support industries seeking consistency, purity, and scalability.
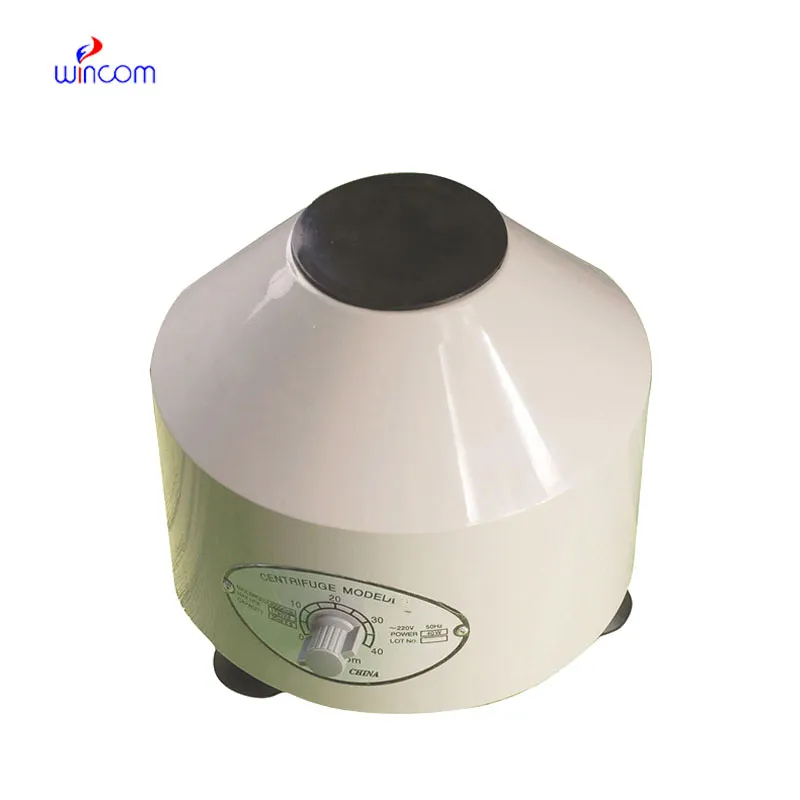
Sustainability, connectivity, and accuracy will be the areas of future evolution of large capacity refrigerated centrifuge manufacturer. Instruments will be made with sustainable materials and energy-efficient drives to minimize their carbon footprint. Real-time monitoring of data through cloud-based systems will facilitate real-time troubleshooting and process optimization. Portable versions will enhance accessibility in remote- or field-based studies. In pharma and biotech, large capacity refrigerated centrifuge manufacturer will ramp up production with intelligent automation. As technology continues to evolve, large capacity refrigerated centrifuge manufacturer will remain at the center of scientific innovation, bridging the gap between mechanical performance and digital intelligence.
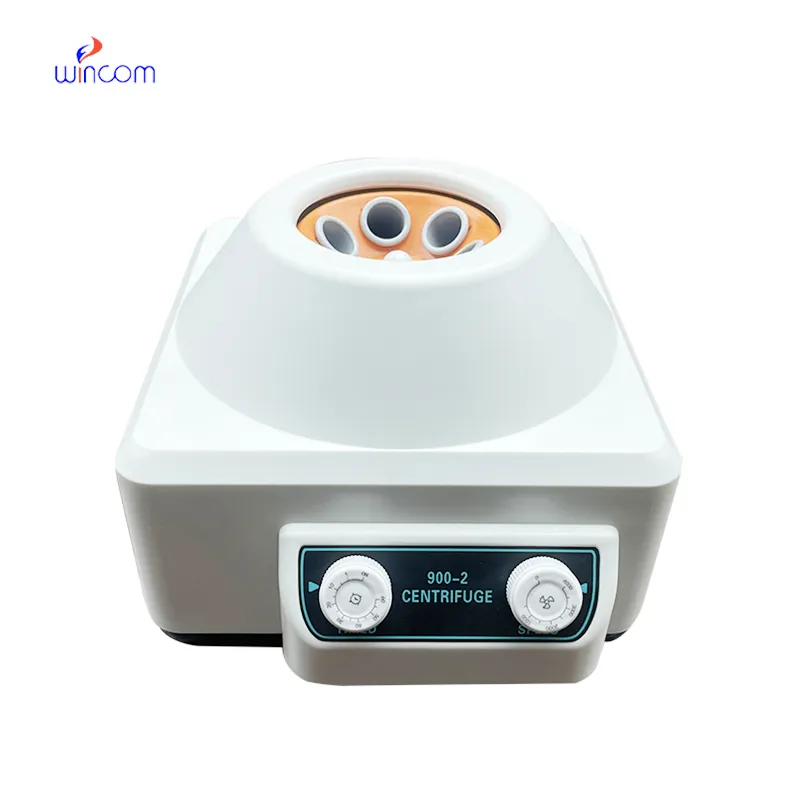
Well-maintained large capacity refrigerated centrifuge manufacturer assure trouble-free operation and optimize equipment longevity. Users must ensure balanced loading to prevent excessive stress to bearings. Regular cleaning of the rotor, chamber, and seals reduces cross-contamination. Regular lubrication and calibration ensure mechanical accuracy. Logs of maintenance, checklists, and other records facilitate quality control and inspection for compliance. Internal humidity and dust exposure should be reduced. Laboratories use preventive maintenance instructions to guarantee that large capacity refrigerated centrifuge manufacturer delivers constant high performance with little downtime and repair.
A large capacity refrigerated centrifuge manufacturer operates by inducing centrifugal force through rapid rotation, separating substances according to mass and density. It has a critical use in laboratories, medical testing, and industrial treatment. In medicine, for instance, large capacity refrigerated centrifuge manufacturer facilitate plasma and serum separation for the purpose of diagnosis. In environmental science, they assist in the examination of suspended solids in water samples. Their robust build, combined with programmable functions and safeguarding features, facilitates fine speed control and timing. large capacity refrigerated centrifuge manufacturer continue to evolve to provide faster and more accurate separation procedures in various fields.
Q: What are the main components of a centrifuge? A: Key components include the rotor, motor, control panel, safety lid, and chamber, each working together to achieve precise separation. Q: How can I verify that a centrifuge is functioning correctly? A: Check that the machine runs smoothly without any unusual vibrations or noises, check the speed accuracy and evaluate the results to ensure consistent separation. Q: Is it safe to open a centrifuge immediately after use? A: No, the device should come to a complete stop before opening to avoid injury or sample disruption. Q: How should a centrifuge be stored when not in use? A:Store it unplugged, covered, and in a dry, dust-free environment to protect internal components from moisture and corrosion. Q: Can centrifuge operation be automated? A: Yes, modern models include programmable controls and digital interfaces that allow automated speed, time, and temperature settings.
The microscope delivers incredibly sharp images and precise focusing. It’s perfect for both professional lab work and educational use.
This ultrasound scanner has truly improved our workflow. The image resolution and portability make it a great addition to our clinic.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We are planning to upgrade our imaging department and would like more information on your mri machin...
Could you share the specifications and price for your hospital bed models? We’re looking for adjus...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China


 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko